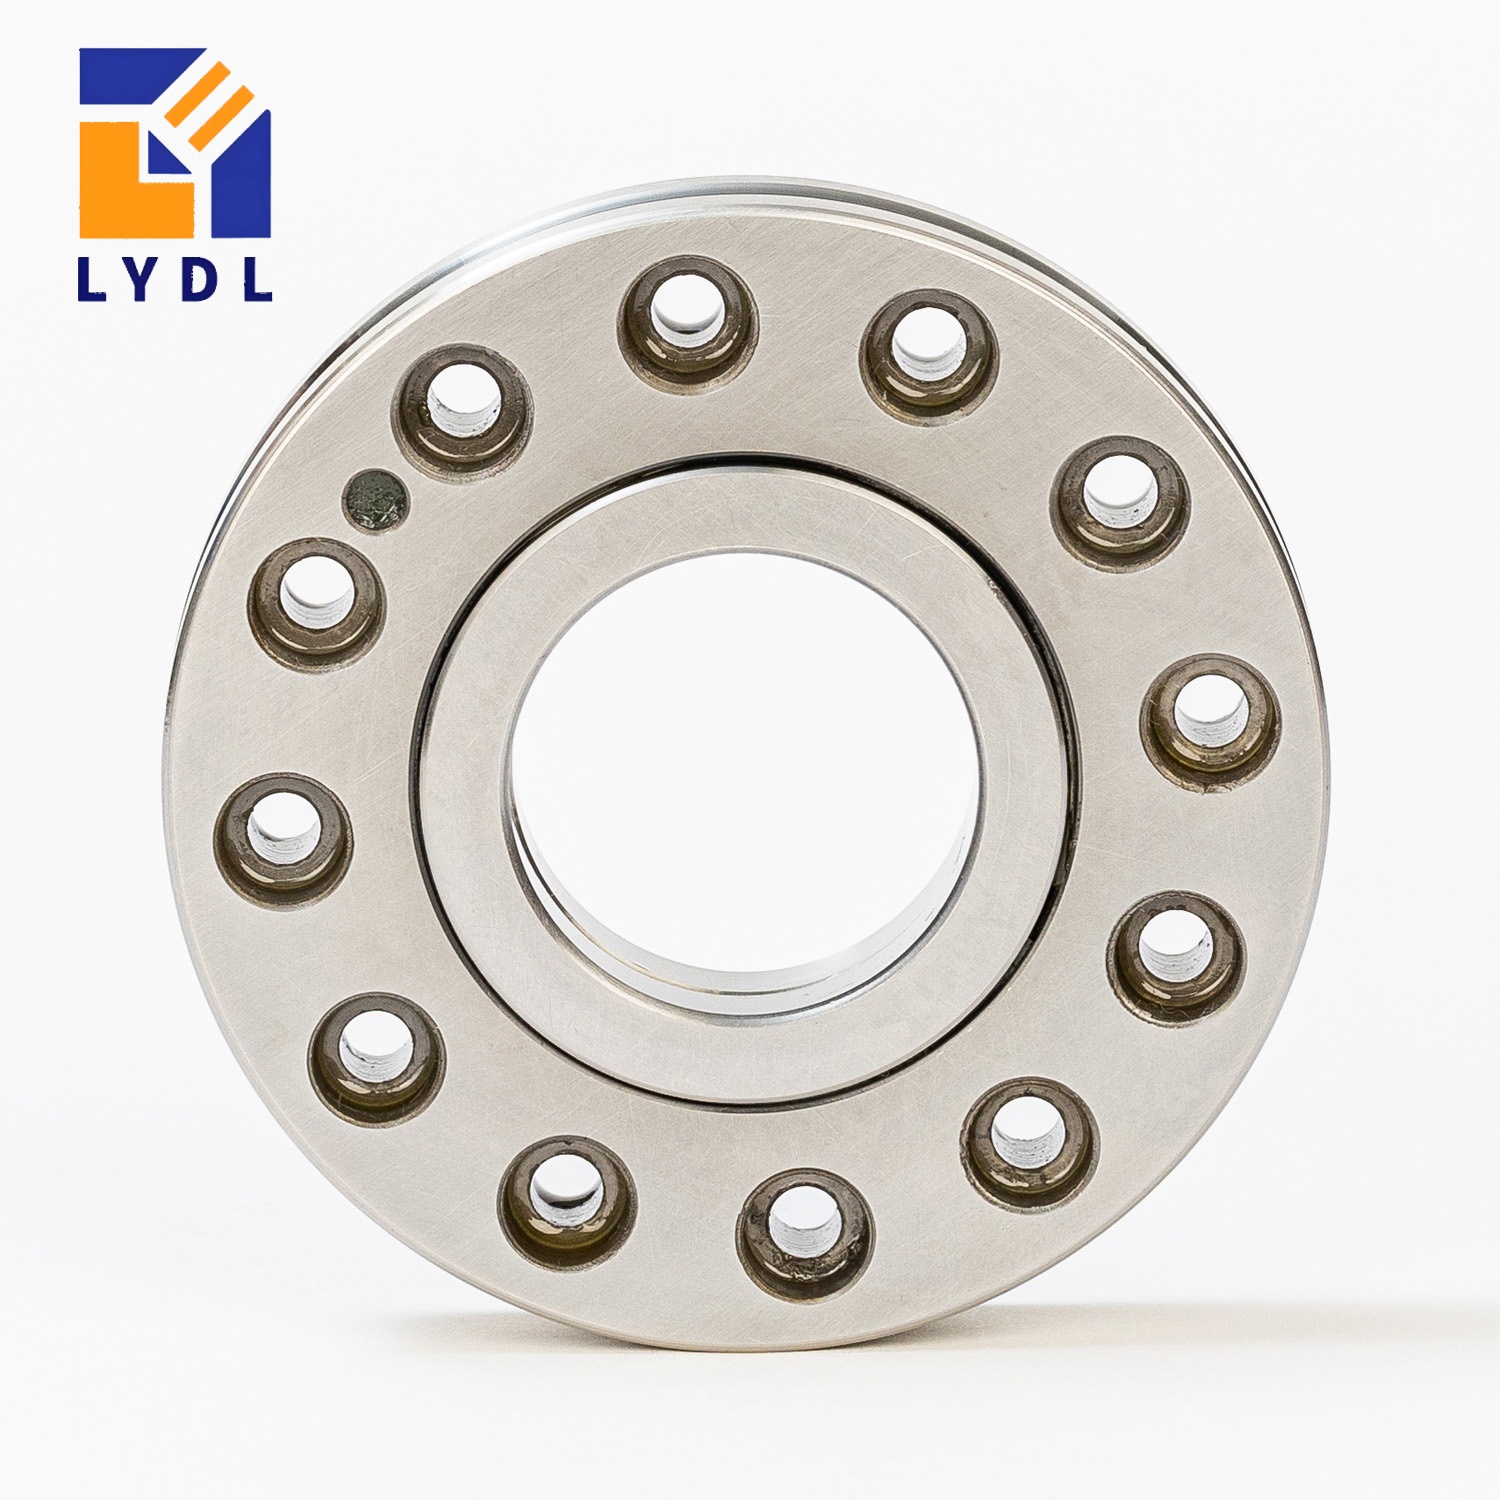
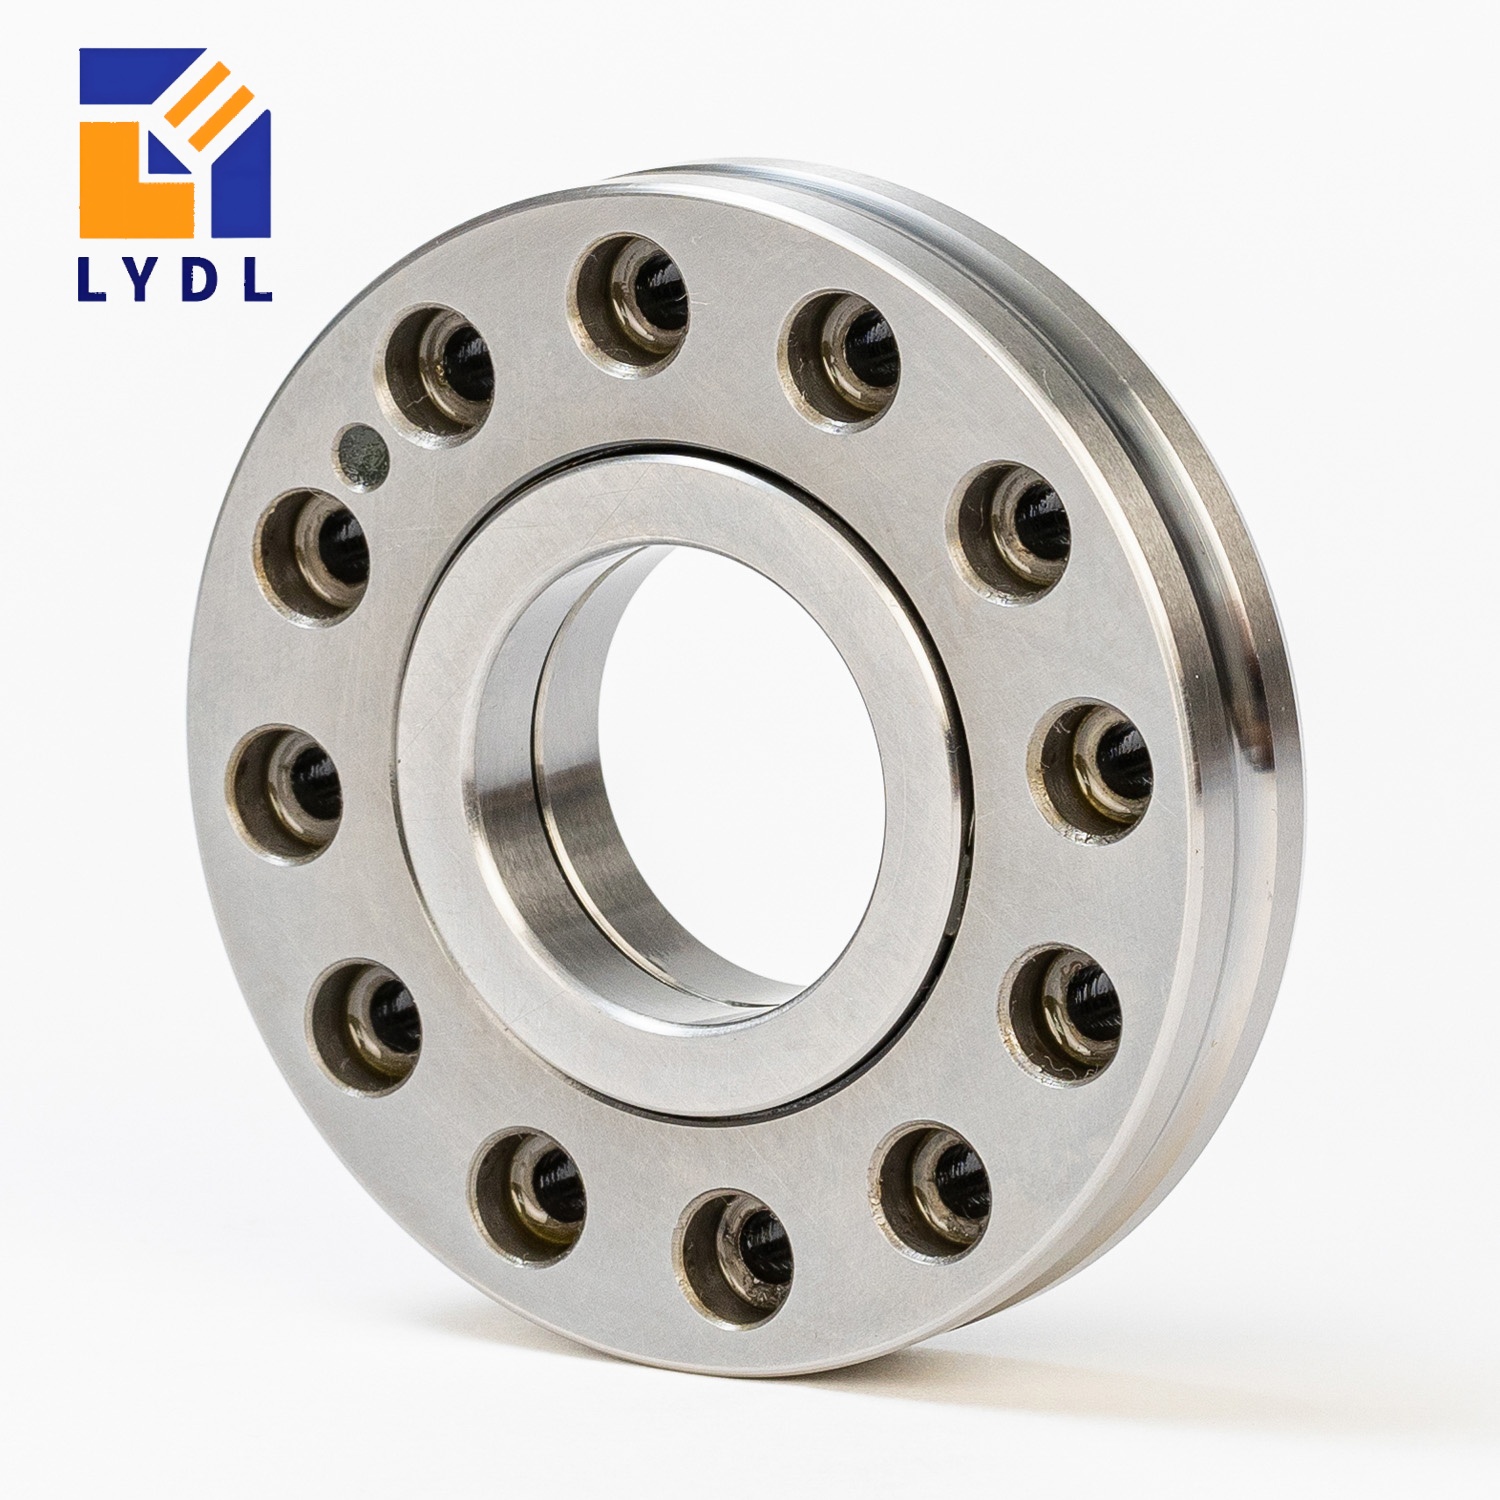
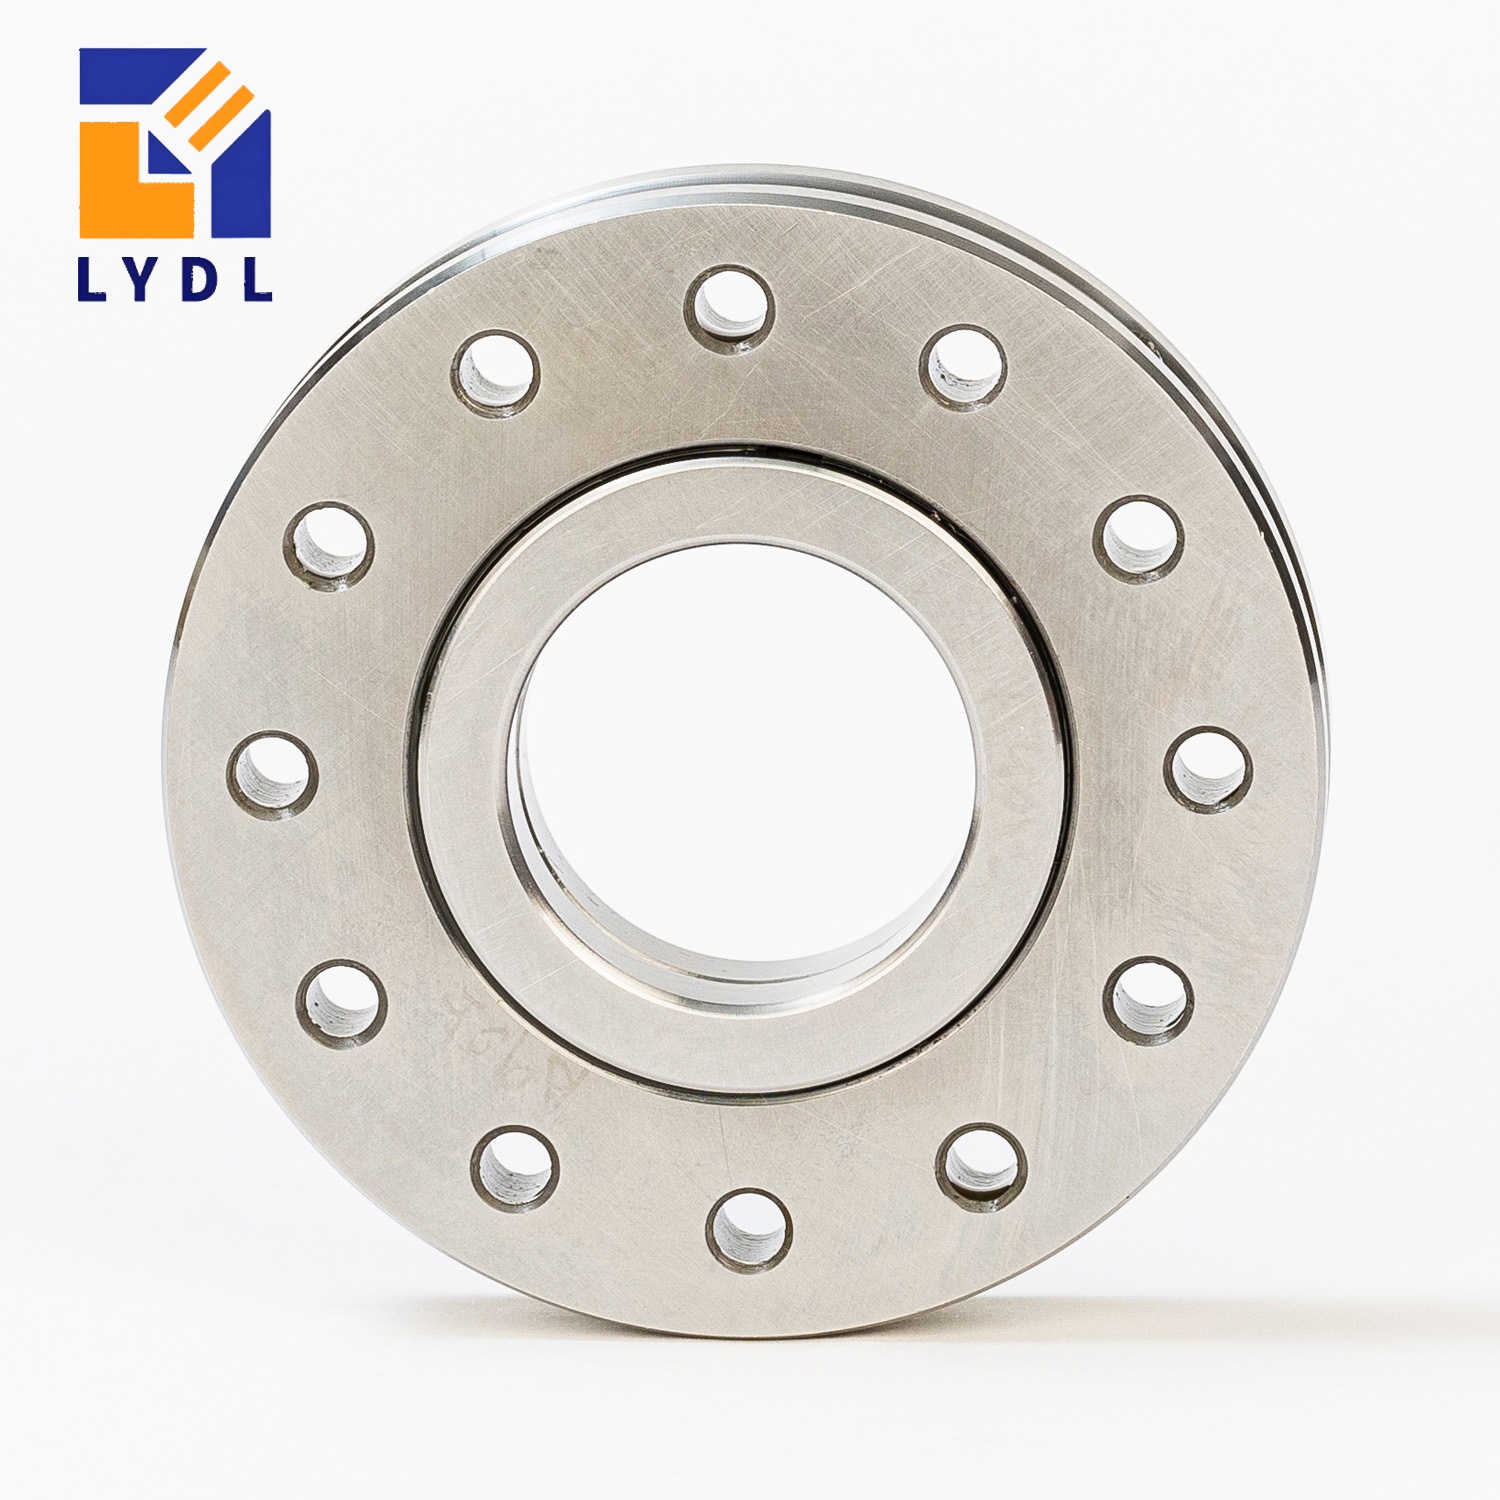
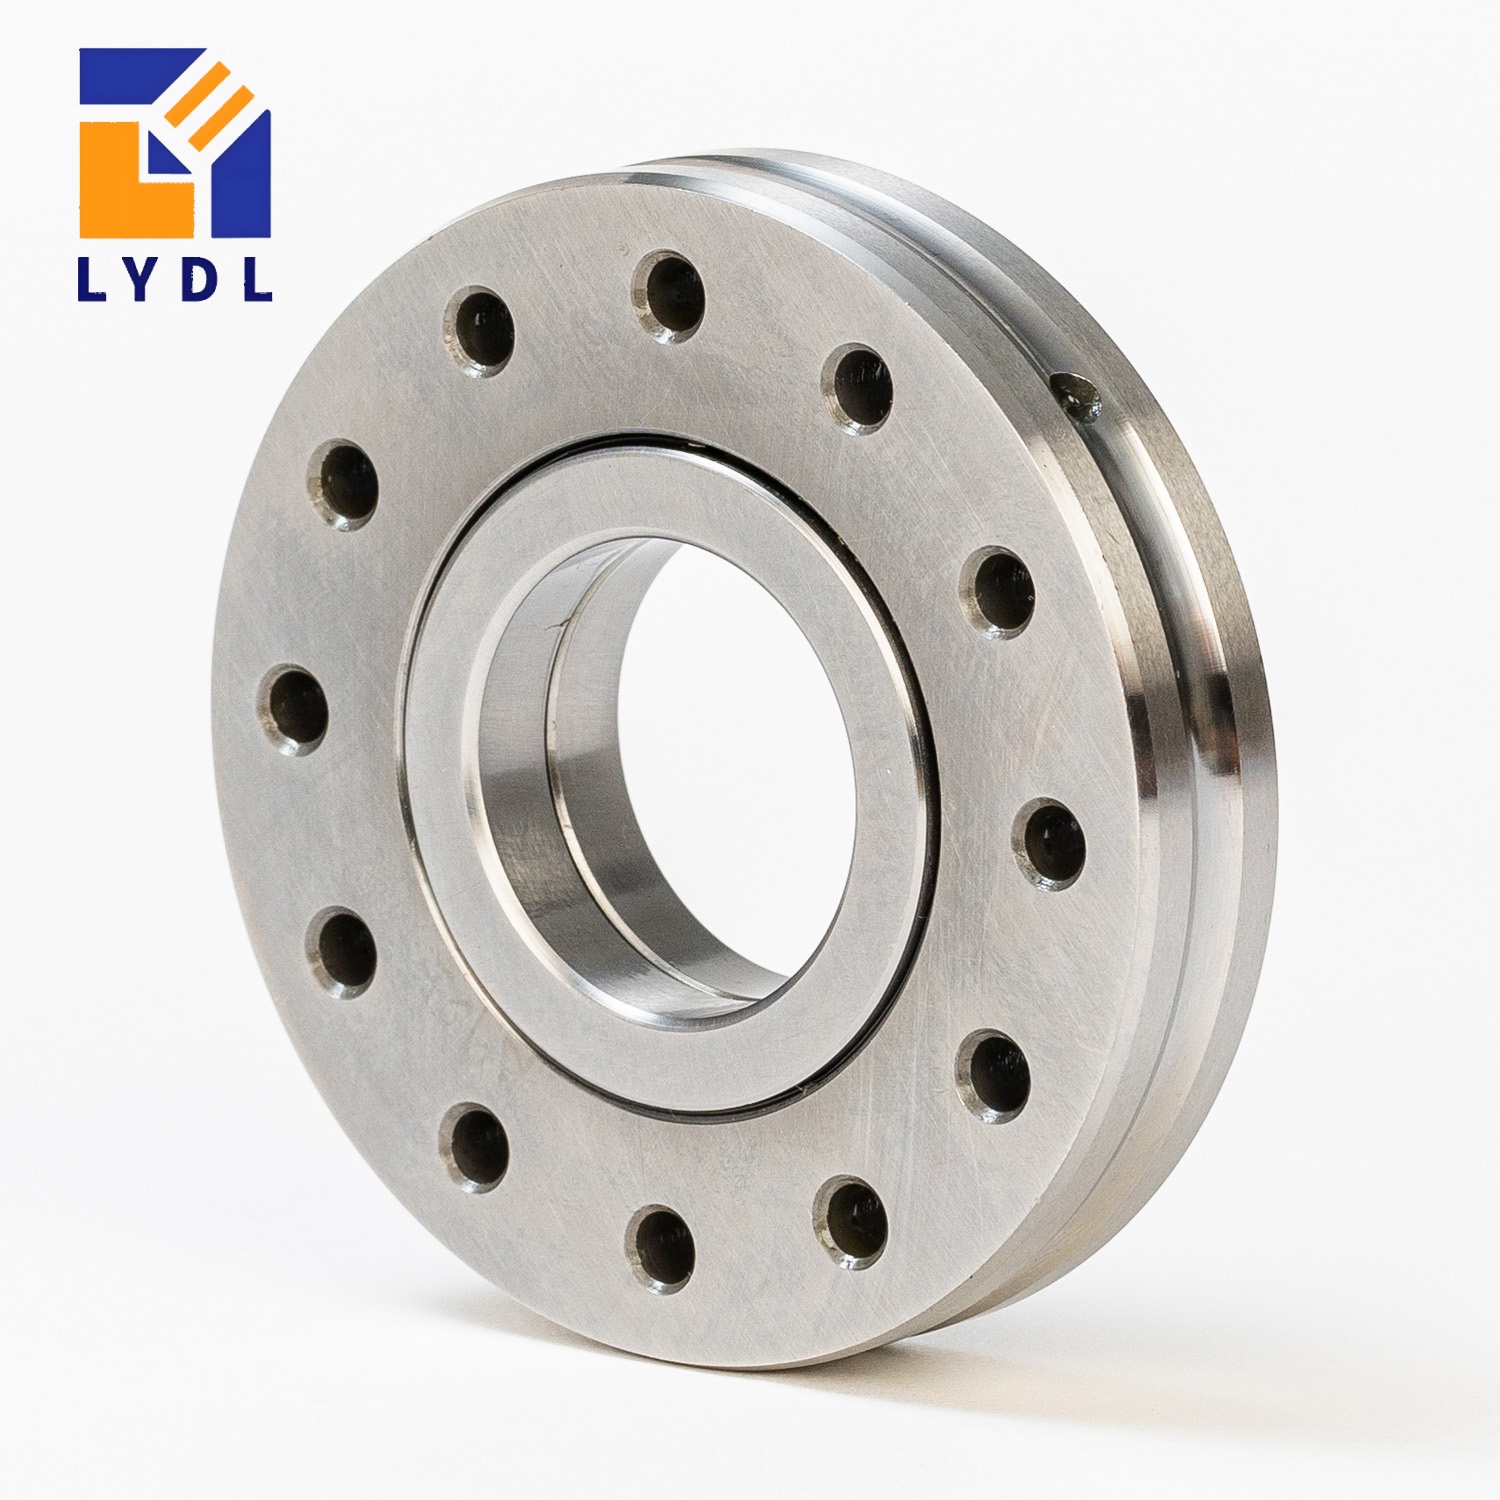
The XV80 crossed roller bearing is a sealed, grease-lubricated precision bearing developed for rotary systems requiring an 80 mm bore, increased load capacity and direct outer-ring mounting.
Dimensions: 80 mm bore × 135 mm outside diameter × 19 mm overall width
Mounting interface: 16 counterbored fixing holes on a 120 mm pitch circle
Fixing-hole dimensions: 6.6 mm through-hole, 11 mm counterbore and 6.4 mm counterbore depth
Ring structure: Solid outer ring with a circumferentially split inner ring
Load capability: Supports radial, axial and overturning-moment loads
Basic dynamic ratings: 33.5 kN axial and 21.4 kN radial
Basic static ratings: 101 kN axial and 40.5 kN radial
Standard configuration: Sealed on both sides, grease lubricated, approximately 1.18 kg
Reference limiting speeds: 402 rpm with preload and 804 rpm with clearance
XV80 is the first standard size in the XV range to use a 19 mm overall width. Compared with XV70, it provides approximately 42% higher dynamic ratings and 44% higher static ratings, making it suitable for more heavily loaded robot axes, gearbox outputs, rotary positioners and precision industrial equipment.
Its solid outer ring can be mounted directly to the adjacent construction, while the split inner ring allows clearance or preload adjustment through an appropriate precision locknut arrangement.
The XV80 crossed roller bearing measures 80 × 135 × 19 mm and provides a higher-capacity step within the compact XV range. Its solid outer ring incorporates 16 counterbored fixing holes on a 120 mm pitch circle, enabling direct attachment to a rigid mounting structure.
The circumferentially split inner ring allows the bearing clearance or preload to be adjusted through a suitable precision locknut arrangement. Cylindrical rollers are arranged alternately at right angles, allowing one bearing position to support radial loads, axial loads in both directions and overturning moments.
XV80 is the first standard XV size with a 19 mm overall width. Compared with XV70, the increased cross-section delivers a substantial improvement in axial and radial load ratings while retaining a relatively compact installation envelope.
Other available dimensions can be viewed in the XV Series Cross Roller Bearings range.
The stated values are catalogue-reference dimensions and basic load ratings. They must not be interpreted as maximum permissible application loads.
Final selection should consider radial and axial loads, overturning moment, acceleration, speed, duty cycle, lubrication, mounting rigidity, temperature and required operating life.
A Higher-Capacity Step from XV70
XV80 is not simply an XV70 with a larger bore. Its wider ring section, larger mounting interface and stronger fixing-hole geometry represent a clear performance step.
Compared with XV70, the XV80 crossed roller bearing provides:
Approximately 42% higher dynamic axial capacity
Approximately 44% higher static axial capacity
Approximately 42% higher dynamic radial capacity
Approximately 45% higher static radial capacity
A larger 80 mm center opening
A larger 120 mm fixing-hole pitch circle
Larger 6.6 mm through-holes and 11 mm counterbores
XV80 is appropriate when XV70 does not provide sufficient bore size or load capacity, but the installation does not require the larger 90 mm bore of XV90.
Solid Outer Ring and Adjustable Inner Ring
The XV80 uses a solid outer ring and a circumferentially split inner ring.
The outer ring can be fastened directly to the adjacent structure through its 16 counterbored holes. This can eliminate a separate outer-ring clamping flange and reduce the number of mounting components.
The split inner ring allows the clearance or preload to be controlled through an appropriate locknut arrangement. Correct adjustment is important because excessive preload can increase torque and temperature, while insufficient preload can reduce rigidity and positioning stability.
For an explanation of different crossed roller bearing structures, see the Cross Roller Bearings Design and Selection Guide.
120 mm PCD and Fixing-Hole Design
The 16 outer-ring fixing holes are equally distributed on a 120 mm pitch circle.
Each fixing position has:
6.6 mm through-hole diameter
11 mm counterbore diameter
6.4 mm counterbore depth
The 6.6 mm through-hole is commonly associated with clearance for an M6-class fastener. However, the selected screw standard, head diameter, engagement length, strength grade and tightening torque must be verified against the approved bearing and housing drawings.
The larger fixing-hole geometry distinguishes XV80 from XV70, which uses 5.6 mm through-holes and 10 mm counterbores.
For reliable installation:
Verify the 120 mm pitch circle before assembly.
Provide continuous support beneath the outer-ring mounting face.
Keep the supporting surface flat and perpendicular to the rotational axis.
Select bolts according to the actual axial and moment loads.
Tighten all bolts gradually in a diagonal sequence.
Recheck running torque and runout after final tightening.
The bearing mounting holes cannot compensate for a flexible plate, uneven surface or insufficient thread engagement.
80 mm Central Opening
The 80 mm bore provides space for a hollow shaft, drive components or internal services such as electrical wiring, pneumatic tubing, sensor cables and optical elements.
The actual usable routing diameter will be smaller than 80 mm after allowing for:
Shaft wall thickness
Precision locknut
Locking or retaining features
Assembly clearance
Cable protection
Shaft-strength requirements
For belt-driven or gear-driven axes, the design must also account for radial belt tension, gear-separation force, shaft deflection and load offset from the bearing center.
The central opening should therefore be evaluated as part of the complete shaft assembly rather than treated as an unrestricted 80 mm passage.
XV80 Compared with RE8016
XV80 and RE8016 both have an 80 mm nominal bore and use a solid outer ring with a split inner-ring concept, but they have different boundary dimensions and mounting methods.
The RE Series Cross Roller Bearings may be considered when a smaller 120 mm outside diameter and 16 mm width are more important than the XV80 direct-mounting interface.
Matching bore diameters do not make the two models interchangeable. The outer diameter, width, supporting surfaces, ring retention, preload arrangement and load ratings must all be verified.
Typical XV80 Applications
The XV80 crossed roller bearing is suitable for precision rotary systems that need an 80 mm central opening, increased rigidity and higher load capacity than the smaller XV models.
Application
Why XV80 May Be Suitable
Main Engineering Check
Industrial robot axes
Higher moment capacity and hollow-axis space
Reversing load and emergency-stop torque
Robot positioners
Direct outer-ring mounting
Payload offset and mounting-plate rigidity
Gearbox output supports
Combined-load capability
Gear forces and shaft alignment
Servo-driven rotary units
Compact precision support
Acceleration and thermal stability
CNC auxiliary axes
Increased static capacity
Cutting-force moment and runout
Inspection turntables
Stable angular support
Running torque and measurement accuracy
Semiconductor equipment
Compact sealed arrangement
Cleanliness and lubricant compatibility
Optical positioning systems
80 mm central passage
Torque variation and angular error
Medical equipment
Compact combined-load support
Material and lubrication requirements
Automated assembly stations
Direct mounting and rigidity
Shock load and cycle frequency
Need an XV80 Selection Review?
Before prototype production, provide the applied loads, speed, duty cycle, shaft drawing and mounting arrangement. The LYDL Engineering and Sales Team can review the required clearance, preload, lubrication and inspection configuration.
Load and Moment Evaluation
Crossed rollers enable XV80 to support radial load, axial load and overturning moment at the same time. However, catalogue ratings cannot be used alone to approve an application.
For an offset load, the basic overturning moment can be estimated using: M = F × L Where:
M is the applied moment
F is the applied force
L is the perpendicular distance from the bearing center
The calculation should also include:
Payload acceleration and deceleration
Emergency stopping
Gear or belt forces
External vibration
Impact or collision loads
Duty cycle
Mounting-structure deformation
Required safety factor
The bearing, fixing screws, inner-ring retention and adjacent structure must be evaluated as one complete load path.
Limiting Speed and Thermal Control
The catalogue-reference limiting speeds for XV80 are:
402 rpm with preload
804 rpm with clearance
These figures are reference limiting speeds rather than recommended continuous operating speeds.
The actual permissible speed may be reduced by:
Higher preload
Heavy combined loading
Frequent acceleration and reversal
Grease type and fill quantity
Limited heat dissipation
Mounting misalignment
High ambient temperature
Seal friction
For positioning equipment, stable running torque and temperature are often more important than the highest possible rotational speed.
Clearance, Preload and Suffix Guidance
The inner-ring condition should be selected according to the required rigidity, positioning accuracy, running torque and temperature.
Common catalogue references include:
Standard clearance: For applications prioritizing lower friction
RL0: Reduced-clearance catalogue reference
VSP: Preloaded-bearing catalogue reference
RR: Corrosion-resistant catalogue reference
Suffix definitions can differ between manufacturers. A designation should not be considered equivalent based only on the base model and suffix.
Before replacing an existing bearing, verify:
Boundary dimensions
Mounting-hole geometry
Accuracy and runout
Internal clearance or preload
Starting and running torque
Sealing and lubrication
Load ratings
Permissible speed
Operating temperature
Inspection requirements
Third-party suffixes and model numbers are used only for technical identification and do not guarantee interchangeability.
Manufacturing and Inspection Control
Depending on the agreed XV80 specification, production and inspection may include:
Raw-material and forging inspection
Precision turning and heat treatment
Raceway grinding and superfinishing
Bore, outside diameter and width measurement
Raceway geometry and roundness inspection
120 mm pitch-circle inspection
Fixing-hole and counterbore measurement
Surface roughness inspection
Hardness verification
Roller sorting and matching
Radial and axial runout inspection
Clearance or preload verification
Starting and running torque testing
Seal and grease inspection
Final cleaning and appearance inspection
Serial-number and packaging verification
For precision applications, the method used to inspect the 120 mm pitch circle, runout and torque should be defined in the approved drawing or technical agreement.
Installation Recommendations
Correct installation is essential for maintaining rigidity, accuracy and consistent running torque.
Keep the bearing packaged until the assembly environment is ready.
Clean the shaft, locknut, support surface and fixing holes.
Check the shaft and mounting dimensions against the approved drawing.
Confirm supporting-face flatness and perpendicularity.
Do not strike the rings or transmit assembly force through the rollers.
Seat the solid outer ring evenly against its supporting surface.
Install the split inner ring with the specified precision locknut.
Adjust the clearance or preload in controlled stages.
Tighten the outer-ring screws gradually in a diagonal sequence.
Rotate the assembly during staged tightening.
Measure final runout and rotational resistance.
Perform a low-speed trial and monitor temperature.
The required locknut torque, bolt torque and fit cannot be determined from the 80 × 135 × 19 mm dimensions alone.
Lubrication and Operating Environment
The standard catalogue design is sealed on both sides and grease lubricated.
Lubrication should be selected according to:
Speed and duty cycle
Preload
Starting-torque requirement
Operating temperature
Contamination level
Maintenance interval
Cleanroom requirements
Compatibility with surrounding materials
The catalogue reference temperature range is −30°C to +80°C. Suitability across this range also depends on the selected grease, seals and adjacent components.
Vacuum, cleanroom, low-temperature, low-outgassing, food-processing, washdown or corrosive environments require separate technical confirmation.
Packaging and OEM Supply
XV80 bearings can be supplied with individual protective packaging, identification labels and reinforced export cartons according to the confirmed order.
Available support may include:
Standard and customized bearing production
Clearance or preload control
Application-specific grease
Dimensional inspection reports
Running-torque records
Customer part-number marking
Batch and serial-number traceability
OEM labels and packaging
Prototype and production quantities
Export documentation
Final marking, lubrication, inspection and packaging requirements should be stated in the purchase specification.
XV80 Frequently Asked Questions
Why does XV80 use a 19 mm width instead of the 17 mm width of XV70?
The larger 19 mm section provides space for a stronger internal load-carrying arrangement and a larger mounting interface. It supports the substantial increase in axial and radial ratings compared with XV70.
How much more load capacity does XV80 provide than XV70?
The catalogue ratings indicate approximately 42% higher dynamic axial and radial capacity and about 44% higher static axial and radial capacity. Application suitability still depends on the complete load spectrum.
Are the 6.6 mm holes designed for M6 screws?
A 6.6 mm through-hole is commonly used as clearance for an M6-class fastener. The 11 mm counterbore, head type, bolt grade, engagement length and tightening torque must still be checked against the approved assembly drawing.
Can the inner ring rotate while the XV80 outer ring remains fixed?
This arrangement is possible and is consistent with many XV installations. The split inner ring must be correctly retained and adjusted, while the outer ring requires rigid and uniform mounting support.
Is XV80 suitable for a belt-driven or gear-driven rotary axis?
It may be suitable, but belt tension, gear-separation force, shaft deflection and the distance between the drive load and bearing center must be included in the calculation.
Does mounting-plate thickness affect XV80 performance?
Yes. A thin or flexible mounting plate can deform under screw preload and external moment load, reducing rigidity and changing running torque or runout. Plate thickness and support geometry should be evaluated with the bearing.
What should be checked after adjusting the precision locknut?
Check axial and radial movement, starting torque, running torque, runout, noise and temperature. The measurements should be repeated after the outer-ring bolts reach their final torque.
Can XV80 be configured for cleanroom equipment?
Potentially, but grease, seal material, cleaning method, particle requirements and packaging must be confirmed before production. A standard industrial configuration should not automatically be treated as cleanroom compatible.
Does the 101 kN static axial rating make XV80 shock-proof?
No. The static rating is a reference value used in bearing calculations. Shock direction, duration, supporting rigidity, screw capacity and allowable permanent deformation must also be evaluated.
What information is required when replacing another 80 mm-bore bearing?
Provide the complete designation, bearing drawing, shaft and housing dimensions, load spectrum, speed, preload or clearance, accuracy, lubrication and operating environment. An 80 mm bore alone is not enough to establish interchangeability.
Why Choose LYDL for XV80 Bearings?
LYDL supplies precision crossed roller bearings for robotics, CNC equipment, automation systems, measuring machinery and specialized rotary mechanisms.
Customers can request:
Drawing and mounting-interface review
Clearance or preload configuration
Precision locknut coordination
Lubrication selection
Runout and torque inspection
Prototype and batch production
Customer-specific marking
Inspection documentation
OEM and export packaging
International delivery support
All final dimensions, tolerances, preload conditions, suffixes and acceptance requirements are governed by the approved drawing, quotation or technical agreement.
Request an XV80 Quotation
For accurate selection and pricing, please provide:
HIWIN – Crossed Roller Bearing Product Information
Third-party brand names, model references and standards are included only for technical identification and general engineering reference. They do not imply affiliation, authorization, endorsement or guaranteed interchangeability. LYDL supply specifications are governed by the approved drawing, quotation and technical agreement.