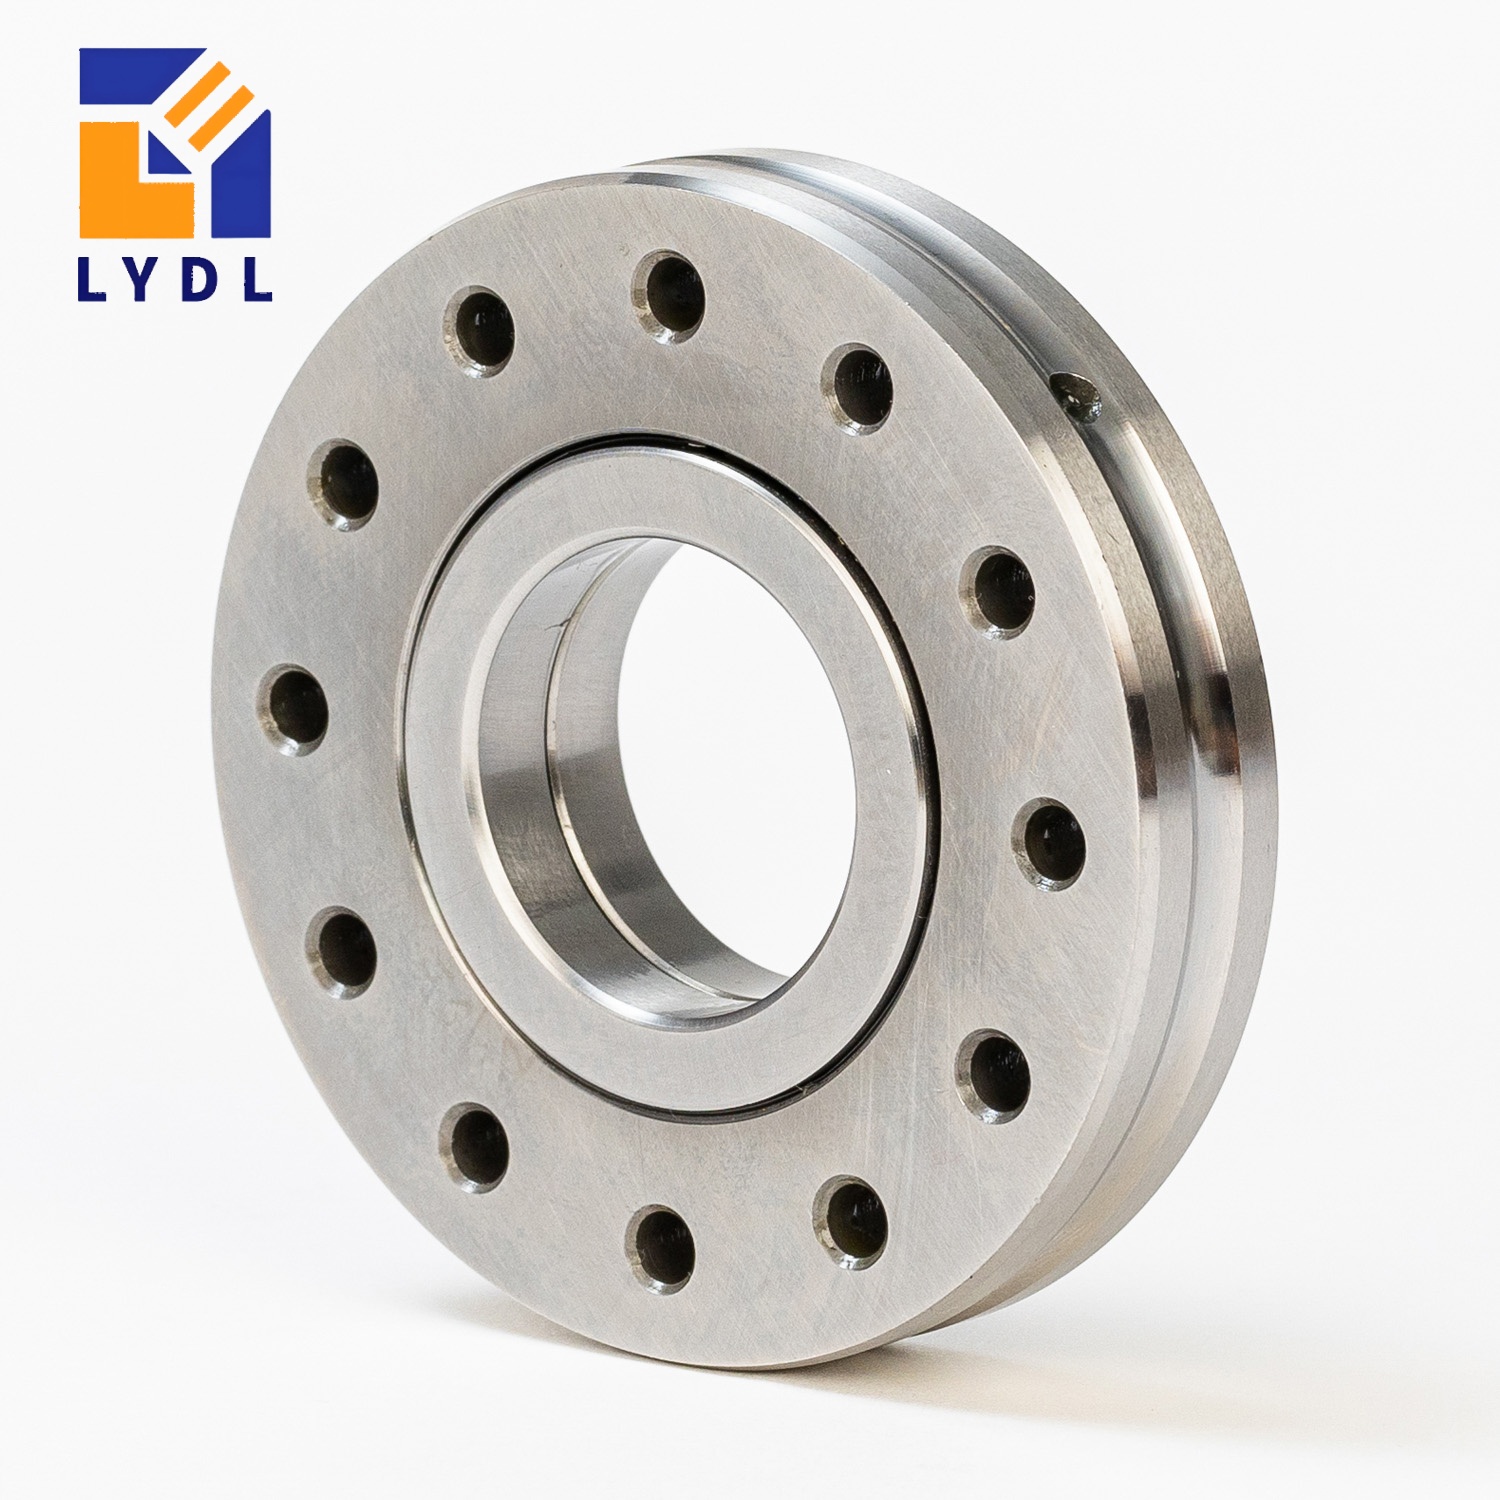
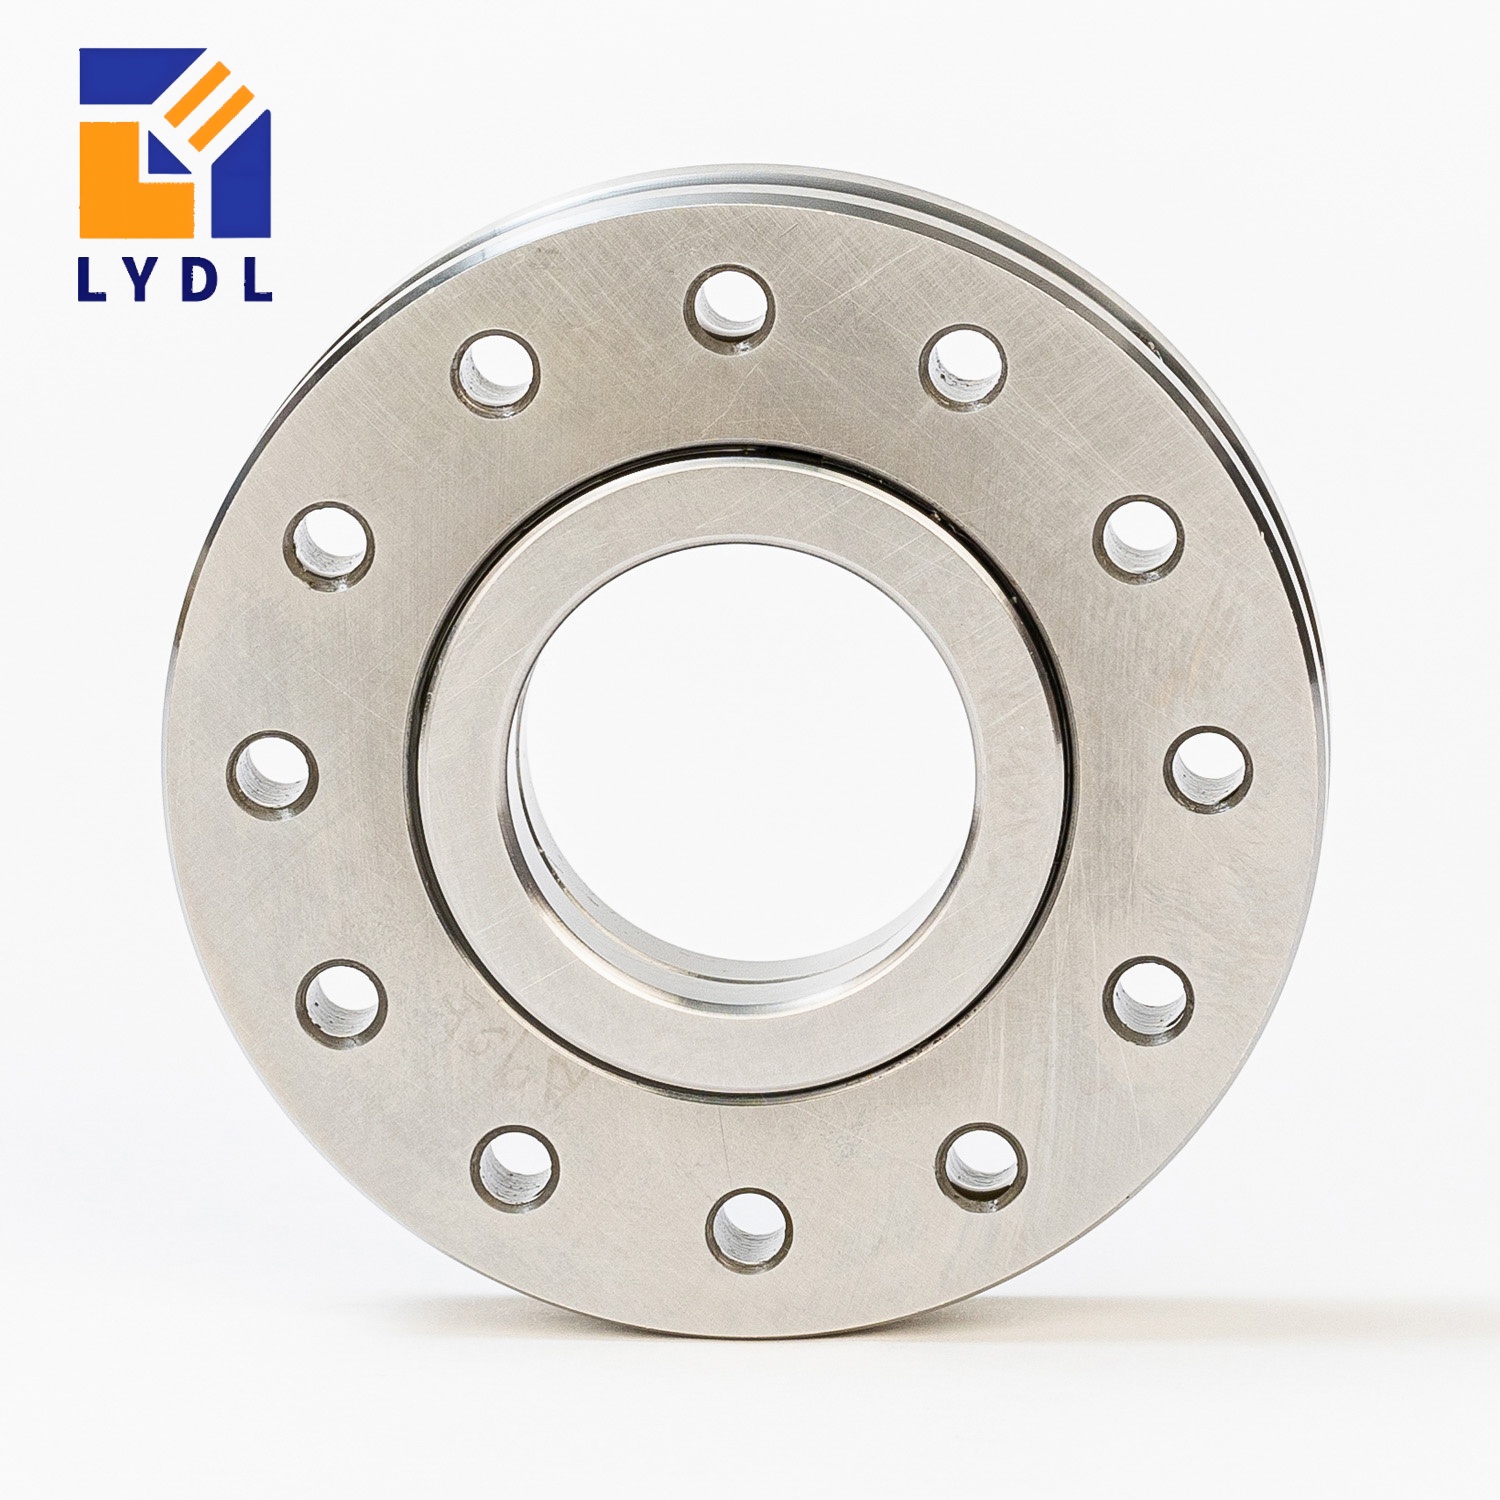
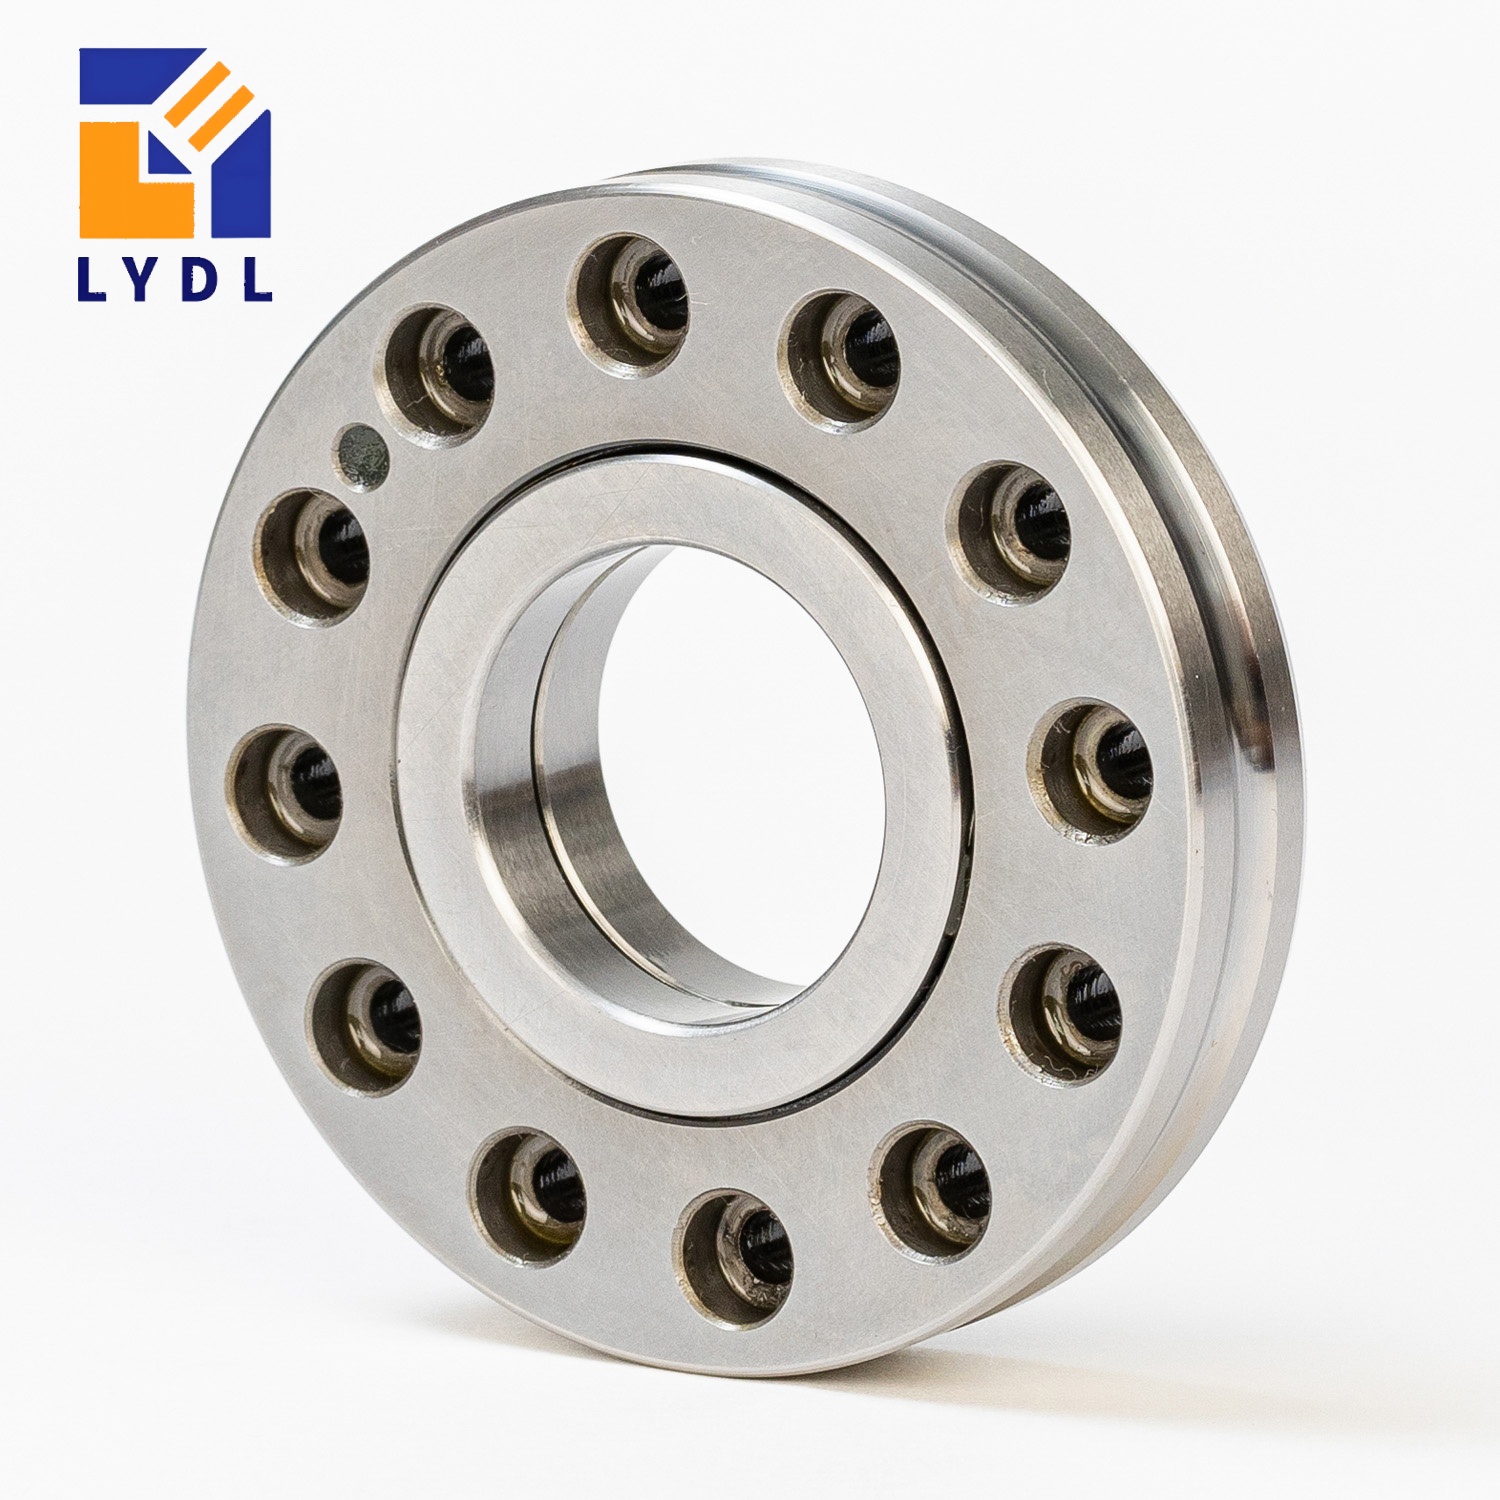
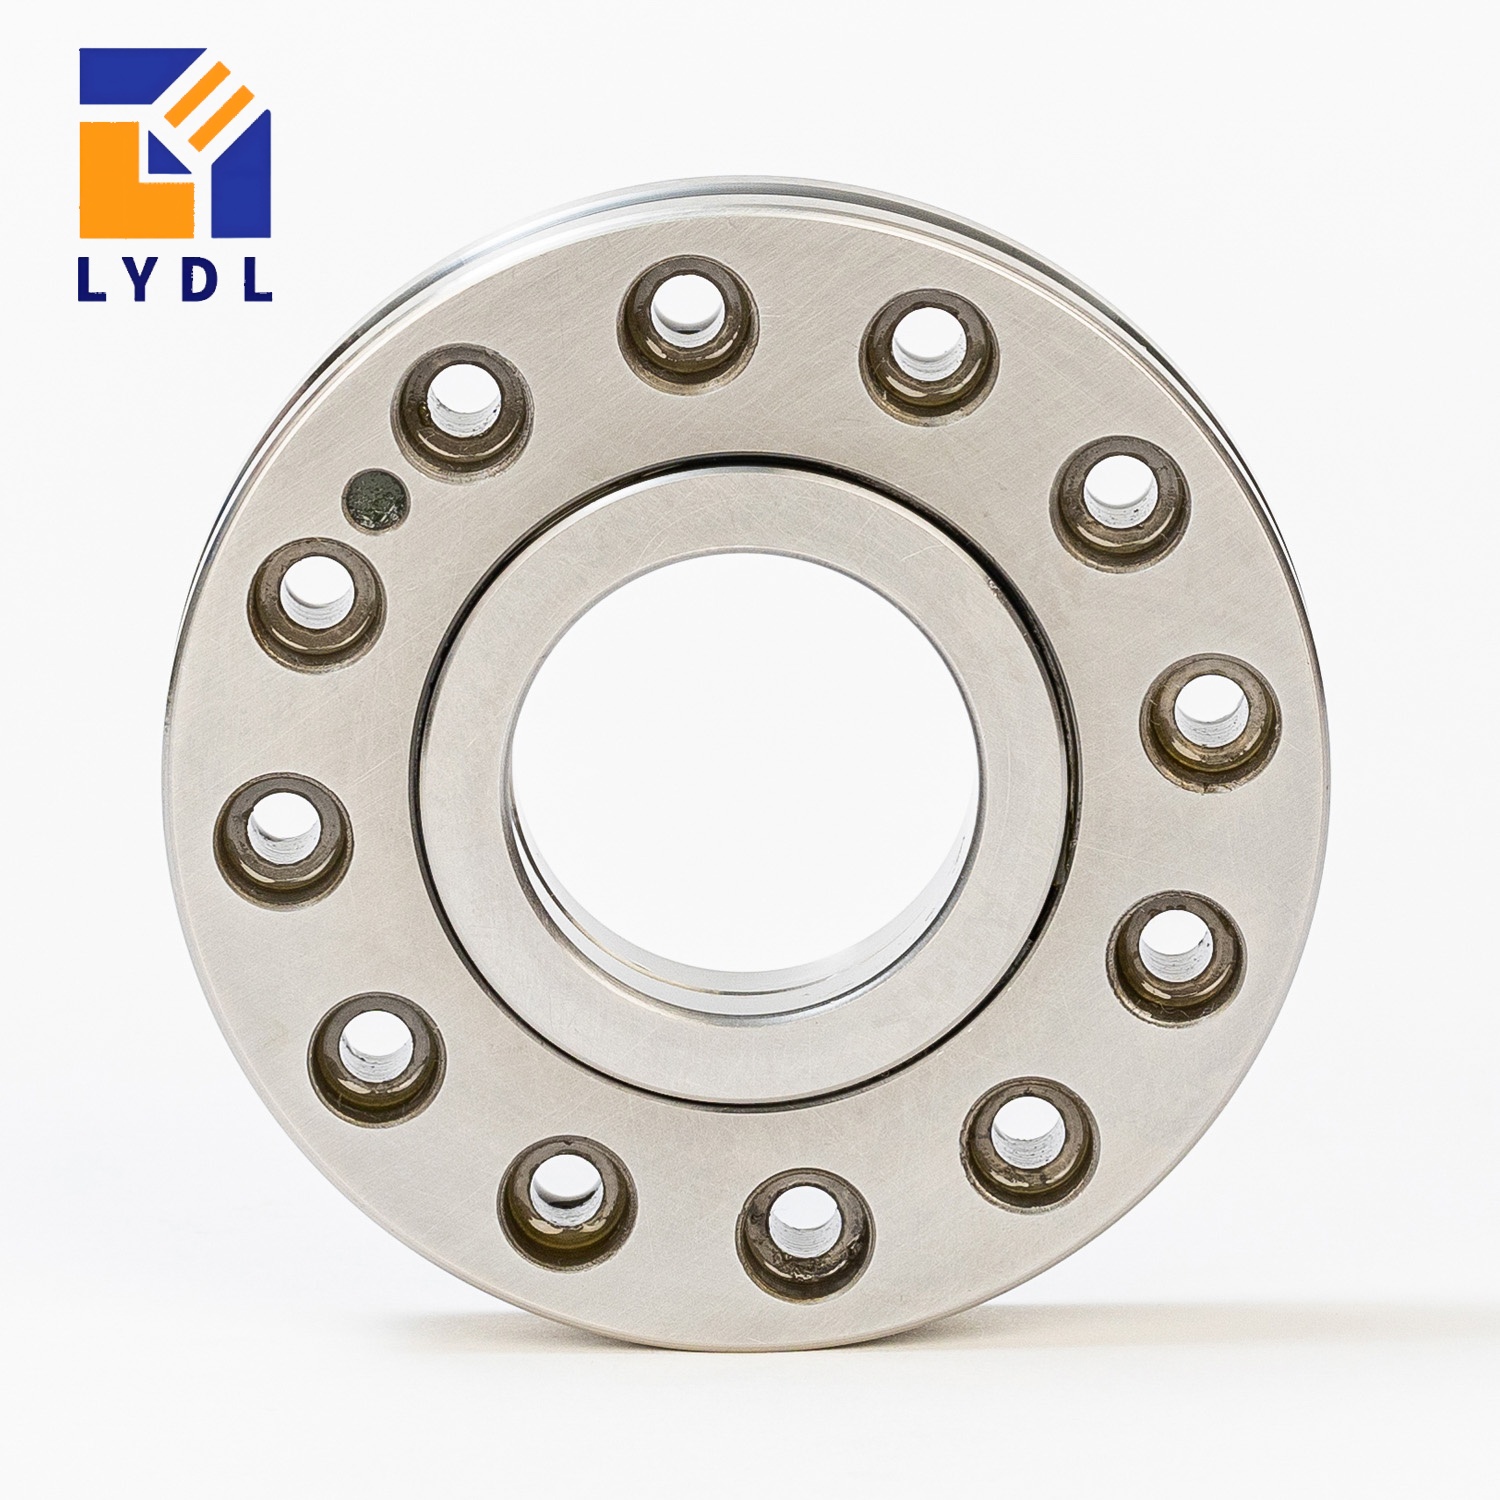
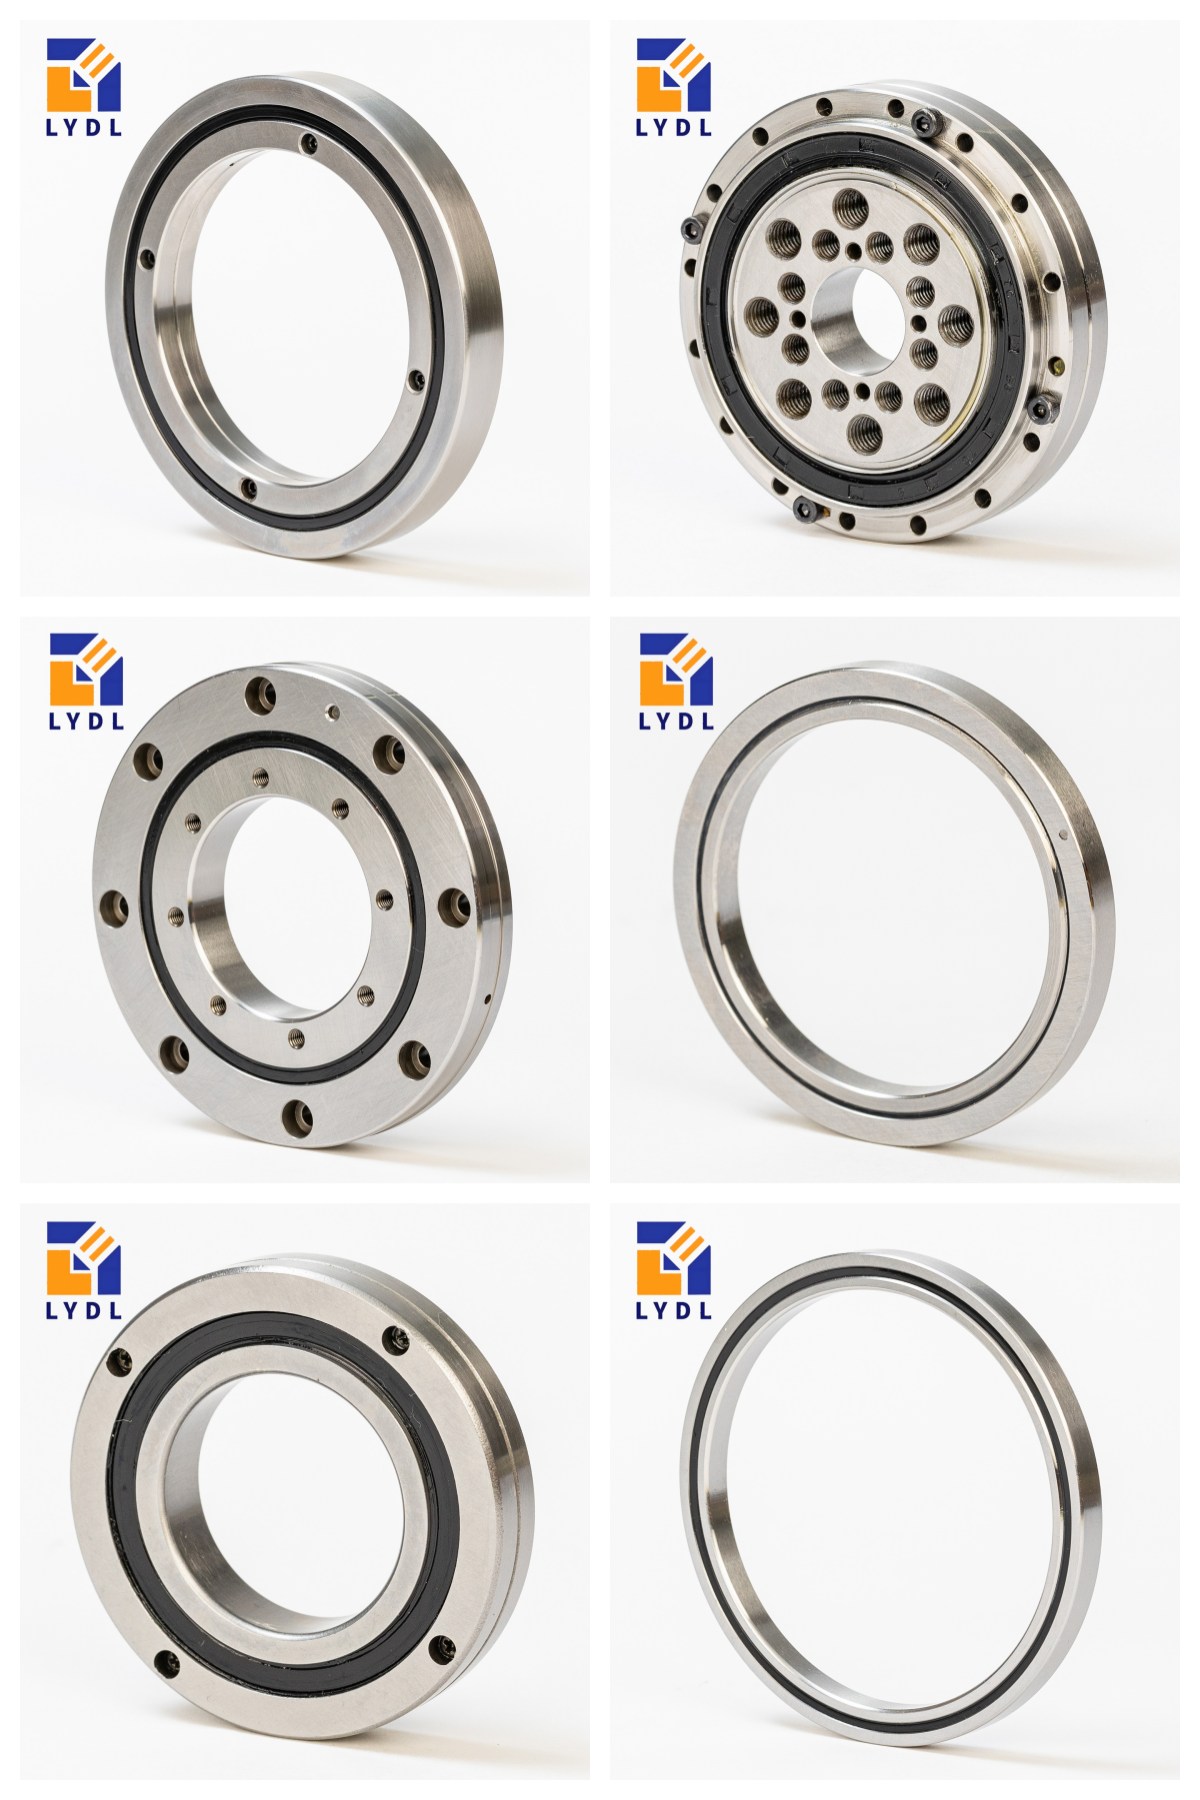
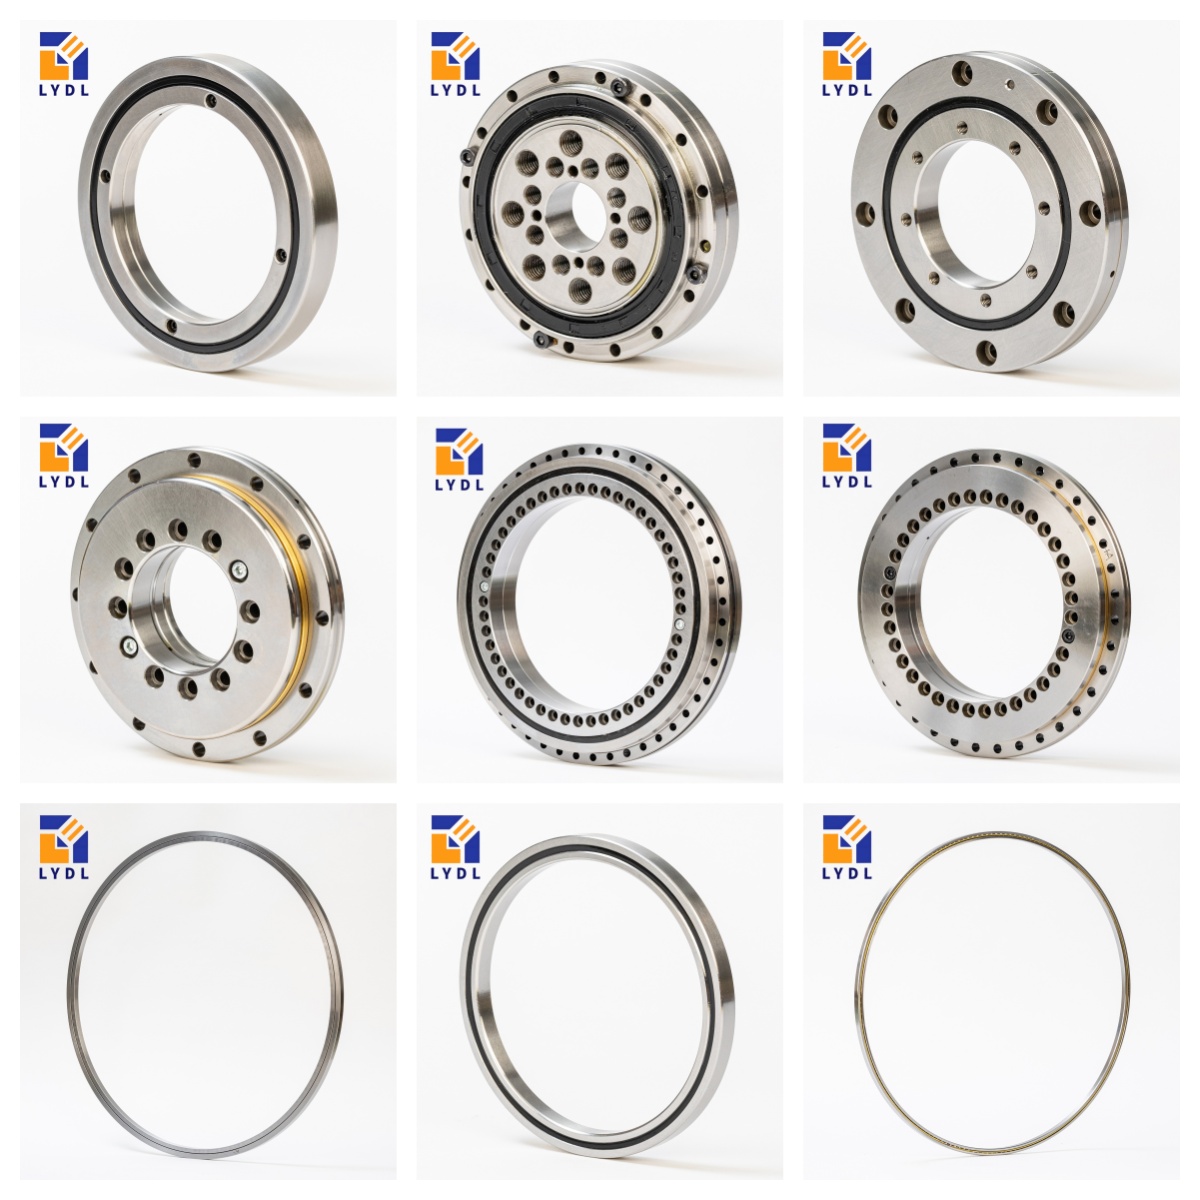
XV30 crossed roller bearing is a compact precision bearing designed for rotary mechanisms requiring high rigidity, smooth rotation and accurate positioning.
Dimensions: 30 mm bore × 75 mm outside diameter × 15 mm overall width
Mounting: 12 counterbored fixing holes on a 60 mm pitch circle for direct outer-ring installation
Structure: Solid outer ring with a circumferentially split inner ring
Load capacity: Supports radial load, axial load in both directions and overturning moment
Standard configuration: Sealed on both sides, grease lubricated and approximately 0.37 kg
The split inner ring can be located and adjusted using a precision locknut, allowing the installed clearance or preload to be controlled according to the application.
LYDL manufactures XV30 bearings for industrial robot joints, precision gearboxes, medical positioning equipment, optical inspection systems, compact rotary modules and automation mechanisms. Low-clearance, preloaded, corrosion-resistant and P5/P4/P2 accuracy configurations can be evaluated according to the approved drawing and inspection requirements.
XV30 crossed roller bearing is a sealed, grease-lubricated precision bearing designed for compact rotary systems that require high rigidity, accurate positioning and multidirectional load capacity. Cylindrical rollers are arranged alternately at 90 degrees in V-shaped raceways, allowing a single bearing to support radial load, axial load in both directions and overturning moment.
Unlike many RB-series crossed roller bearings, the XV30 uses a solid outer ring with counterbored fixing holes for direct connection to the surrounding structure. Its circumferentially split inner ring is located on the shaft and can be secured and adjusted using a precision locknut. This structure helps simplify installation while providing control over the bearing’s installed clearance or preload.
XV30 is the smallest standard size in the XV series. Its compact 30 × 75 × 15 mm envelope makes it suitable for robot joints, precision gearboxes, medical equipment, measuring instruments, optical systems and small industrial rotary modules.
Why the XV30 Structure Matters
Direct outer-ring mounting: Twelve counterbored holes allow the solid outer ring to be screwed directly to the adjacent structure.
Adjustable installed condition: The split inner ring can be positioned and adjusted using a suitable precision locknut.
Multidirectional load capacity: One bearing position supports radial load, bidirectional axial load and overturning moment.
High stiffness in a compact envelope: Crossed cylindrical rollers provide a rigid arrangement without requiring two separate bearing positions.
Ready for installation: Standard configurations are sealed on both sides and supplied with grease.
XV30 Technical Specifications
Parameter
XV30 specification
Bearing type
Crossed roller bearing
Bore diameter, di
30 mm
Outside diameter, Da
75 mm
Outer-ring width, Ha
14 mm
Inner-ring/overall width, hi
15 mm
Inner-ring shoulder diameter, Di
42.5 mm
Mounting diameter, da
41.5 mm
Outer-ring fixing holes
12
Fixing-hole pitch circle
60 mm
Through-hole diameter, dB
4.6 mm
Counterbore diameter, ds
8 mm
Counterbore depth, ts
4.6 mm
Approximate mass
0.37 kg
Permissible radial load, Fr perm
5 kN
Basic dynamic axial load rating, Ca
11.6 kN
Basic static axial load rating, C0a
26 kN
Basic dynamic radial load rating, Cr
7.4 kN
Basic static radial load rating, C0r
10.4 kN
Reference limiting speed, preloaded
910 rpm
Reference limiting speed, with clearance
1,819 rpm
Sealing
Sealed on both sides
Lubrication
Grease lubricated
Standard reference temperature range
−30°C to +80°C
The figures above are reference catalog values. Final dimensions, tolerances, clearance or preload, accuracy grade, lubricant, inspection method and acceptance criteria are governed by the approved LYDL drawing and purchase order.
The limiting speed is not automatically the recommended continuous operating speed. Actual allowable speed depends on load, preload, lubrication, heat dissipation, mounting accuracy and operating cycle.
Load Capability and Bearing Selection
The XV30 can carry radial force, axial force from either direction and overturning moment at the same bearing position. Correct selection should consider the complete load condition, including:
Radial load
Axial load and its direction
Applied moment
Load eccentricity
Rotational or oscillating speed
Duty cycle
Required service life
Required rotational accuracy
Surrounding-component rigidity
Shock, vibration and temperature
Do not select the bearing using only one catalog load rating. The rigidity of the housing, shaft, locknut and mounting screws affects load distribution and installed accuracy. When the outer ring is bolted directly to the adjacent structure, both the raceway and the fixing screws must be considered during application review.
Typical XV30 Applications
Application
Why XV30 is suitable
Industrial robot joints
Compact size, high moment stiffness and accurate positioning
Precision gearboxes
Supports combined loads in a single bearing position
Machine-tool mechanisms
High rigidity and controlled rotational accuracy
Medical equipment
Compact construction and smooth positioning capability
Optical and metrology systems
Low deflection and precise angular movement
Automation and handling equipment
Direct mounting and multidirectional load capacity
Solid outer ring with fixing holes and split inner ring
Suitable when the outer ring is mounted directly and inner-ring adjustment is required
RB3010-type
Split outer ring and integrated inner ring
Often selected when inner-ring rotational accuracy and a conventional housing fit are required
XSU-type
Integrated rings with fixing holes
Suitable for direct mounting where a compact, ready-to-install arrangement is preferred
XV30 is not a direct dimensional replacement for RB3010, RU, XU or XSU bearings. Although these bearings can serve similar precision-rotation applications, their dimensions, mounting interfaces, ring structures, fixing holes and adjustment methods differ.
Always confirm interchangeability using an approved installation drawing.
The XV series covers bore diameters from 30 mm to 110 mm. LYDL can help select the appropriate size based on available space, load, moment, speed and accuracy requirements.
Corrosion-resistant configuration or treatment reference
XV30 VSP RR
Preloaded, corrosion-resistant configuration
XV30 P5/P4/P2
LYDL accuracy requirement specified by drawing and inspection standard
Custom grease or low-torque version
Application-specific and order-defined
OEM marking version
Customer-specific label, marking and packaging
Suffix definitions and availability can vary by manufacturer. Final suffix meaning must be confirmed on the LYDL quotation, technical drawing and order confirmation.
Materials, Accuracy and Customization
LYDL can manufacture or configure XV30 crossed roller bearings according to application requirements, including:
Bearing steel equivalent to GCr15, 100Cr6 or SAE 52100
Standard, P5, P4 or P2 accuracy requirements
Specified radial clearance or preload
Low-torque or high-rigidity assembly
Selected grease for temperature, speed or clean operating conditions
Corrosion-resistant surface treatment
Customer-specific laser marking
OEM labels, cartons and export packaging
Dimensional, torque, accuracy and traceability reports
Accuracy grades should be defined together with the measured items, datum system, inspection method and acceptance criteria. The installed accuracy of the complete mechanism also depends on the shaft, housing, shoulder, locknut and assembly process.
LYDL Manufacturing Process
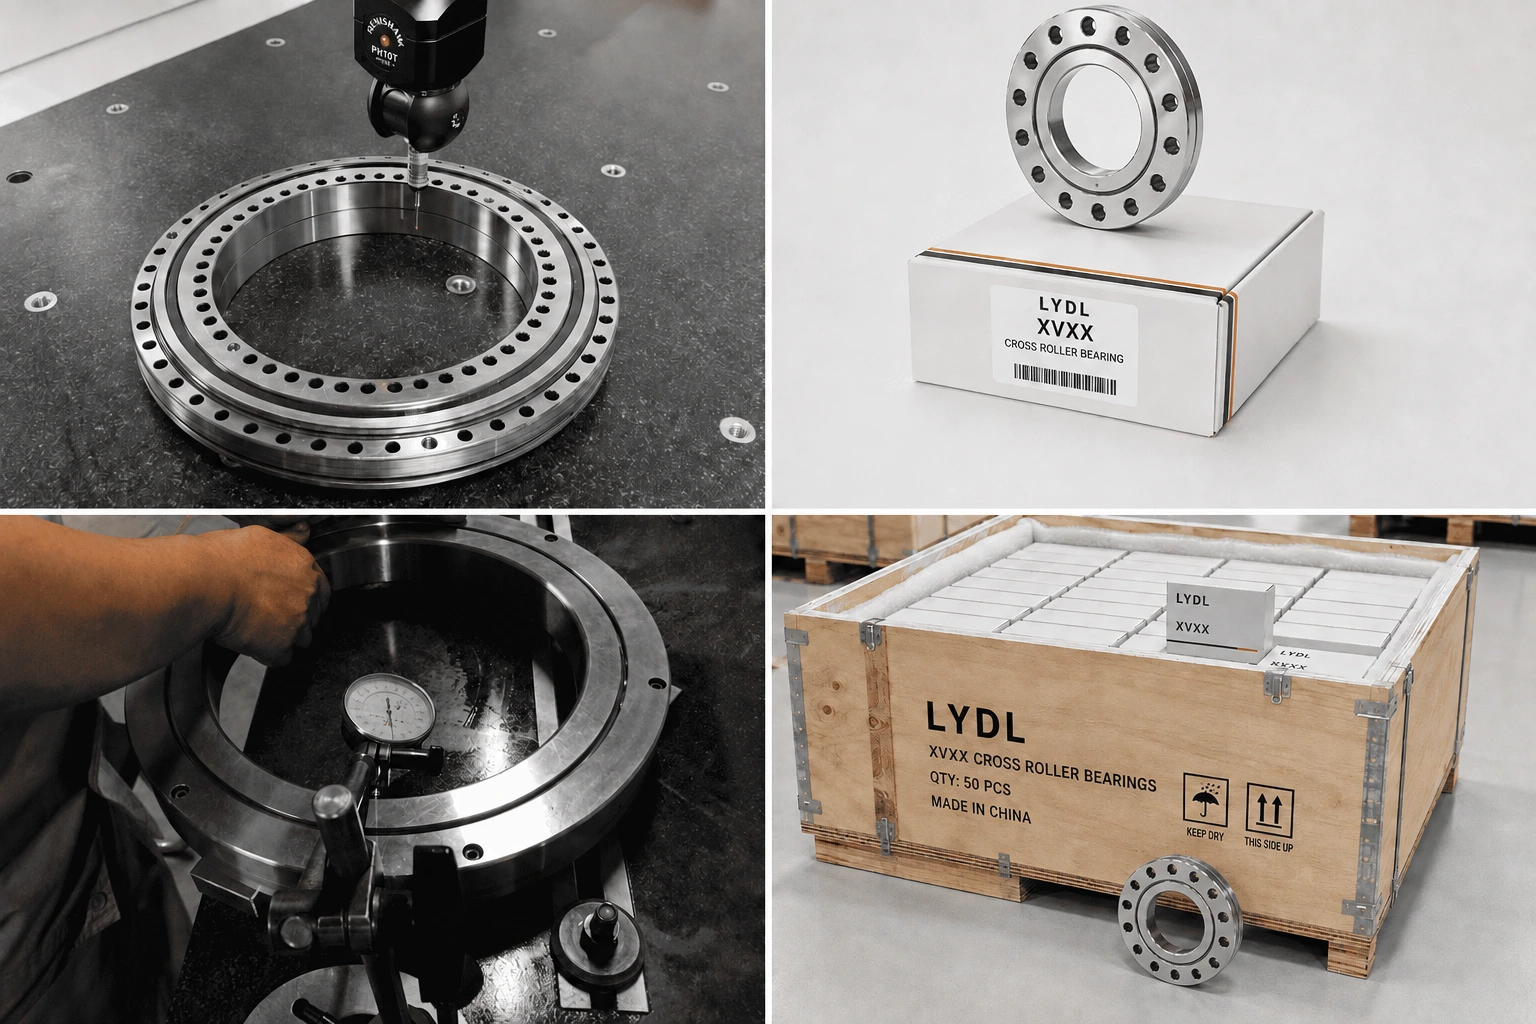
Raw material and forging inspection
Precision soft turning of the rings
Controlled heat treatment and dimensional stabilization
Precision grinding of reference surfaces
Raceway grinding and superfinishing
Roller inspection, micro-sorting, cleaning and demagnetization
Controlled assembly of rollers, spacers, split inner ring, seals and grease
Verification of clearance or preload, rotation torque, runout and dimensions
Laser marking, corrosion protection, packaging and final release
Controlled roller sorting and raceway finishing help maintain uniform internal load distribution, stable rotation torque and repeatable bearing performance.
Inspection and Quality Control
Each production batch is inspected according to the agreed technical requirements. Depending on the order, inspection can include dimensional verification, bore and outside-diameter measurement, width variation, mounting-hole position, radial and axial runout, rotational torque, clearance or preload, surface quality and visual inspection.
For high-precision applications, LYDL can provide inspection records based on agreed measurement datums and acceptance criteria. Customers requiring material certificates, Certificates of Conformity, lubricant information, traceability documents or special inspection reports should specify these requirements before quotation.
Installation and Preload Adjustment
Confirm the approved mounting drawing and bearing orientation.
Remove burrs and clean the shaft, shoulder, mounting surface, screws and locknut.
Apply installation force through the ring being fitted. Do not transfer force through the rollers.
Tighten the outer-ring fixing screws gradually in a diagonal or crosswise sequence.
Support and locate the split inner ring using the specified shoulder and precision locknut.
Set the required clearance or preload using the approved measurement method.
Recheck runout, rotation torque, starting torque and operating temperature after assembly.
Important: A generic locknut tightening torque is not sufficient to define the correct bearing preload. The final setting should be verified using the measurement procedure specified for the machine, such as rotational torque, displacement, clearance or preload measurement.
Uneven mounting surfaces, excessive screw tightening, poor shoulder perpendicularity or unsuitable locknut adjustment can deform the bearing and increase torque, noise, heat generation and runout.
Lubrication, Maintenance and Operating Temperature
The standard XV30 configuration is sealed on both sides and supplied with grease. Reference catalog operating temperature is −30°C to +80°C. Applications outside this range require confirmation of the seals, grease, ring material, surface treatment and surrounding components.
Relubrication requirements depend on speed, load, temperature, oscillation angle, contamination and service life. Overfilling can increase torque and temperature, while insufficient lubrication can shorten bearing life.
If the installation includes lubrication holes or ducts, their positions must be coordinated with the bearing drawing and the machine’s lubrication system.
Packaging and Shipping
LYDL precision bearings are protected against corrosion, impact and contamination during storage and transportation. Packaging can include:
Individual protective wrapping
Model and traceability label
Individual product box
Moisture and anti-rust protection
Foam or shock-resistant separation
Reinforced export carton
Fumigation-free wooden case
Customer-specific OEM packaging
Courier, air freight, sea freight and customer-appointed forwarding arrangements are available according to order quantity and destination.
OEM and Custom Service
LYDL supports distributors, machinery manufacturers, automation integrators and replacement-bearing customers. OEM services can include customer branding, private labels, customized cartons, application-specific grease, corrosion-resistant treatment, selected clearance or preload, accuracy inspection and batch traceability.
For non-standard requirements, please provide the installation drawing, expected quantity, annual demand and technical acceptance criteria.
Frequently Asked Questions About XV30
How is XV30 clearance or preload adjusted?
The split inner ring is located and adjusted using a suitable precision locknut. The final condition should be verified using the approved torque, displacement, clearance or preload measurement procedure. Locknut tightening torque alone does not accurately define the internal preload.
Can LYDL XV30 directly replace INA XV30?
LYDL can evaluate an equivalent solution, but direct replacement must be confirmed by drawing. Bore, outside diameter, width, fixing-hole positions, centring surfaces, clearance or preload, accuracy, seals, lubricant and mounting method should all be checked before installation.
Why does housing accuracy affect installed performance?
The solid outer ring is screwed directly to the adjacent structure. Flatness errors, burrs, uneven screw tightening or insufficient structural rigidity can distort the outer ring and affect rotational torque, runout and internal load distribution.
Is XV30 suitable for outer-ring rotation?
It may be suitable, but the centrifugal effect, screw loading, lubrication, speed, load direction, mounting rigidity and heat generation must be evaluated. Send LYDL the operating conditions for confirmation.
What is the difference between RL0 and VSP?
RL0 generally indicates a low-clearance configuration, while VSP indicates a preloaded configuration. Preload can improve rigidity but may increase rotational torque and heat generation. Final suffix definitions must be confirmed with the supplier.
How should overturning moment be included in bearing selection?
Provide the radial load, axial load, eccentricity, applied moment, speed, duty cycle and required service life. The review should consider both bearing raceway capacity and outer-ring fixing-screw loading.
Can LYDL supply P4 or P2 accuracy?
P4 or P2 requirements can be evaluated when the measured characteristics, measurement datums, inspection method and acceptance limits are clearly defined. Bearing accuracy alone does not determine the installed accuracy of the complete machine.
What documents can be supplied with XV30?
Available documents can include a 2D drawing, dimensional inspection report, material certificate, Certificate of Conformity, accuracy or torque report, lubricant information and batch traceability record. Required documents should be listed before quotation.
Why Choose LYDL for XV30 Crossed Roller Bearings
Manufacturer-focused technical and production support
Application review based on load, speed, moment and installation
Controlled clearance and preload options
P5, P4 and P2 accuracy requirements available for evaluation
Precision raceway finishing and controlled roller assembly
Inspection and traceability documentation
OEM marking, labels and packaging
Support for samples, small batches and production quantities
Drawing confirmation before production
Request an XV30 Quotation
To receive an accurate quotation, please provide:
Required model and quantity
Radial, axial and moment loads
Rotational or oscillating speed
Operating temperature
Required life
Accuracy requirement
Clearance or preload requirement
Lubricant or corrosion-protection requirement
Installation drawing, if available
Required inspection and certification documents
Contact LYDL for an XV30 drawing, technical review, sample order or production quotation.
Technical References and Disclaimer
Primary technical reference: Schaeffler/INA – Crossed Roller Bearings for High Precision Applications General bearing calculation and tolerance references include ISO 281 and ISO 492, where applicable.
INA, Schaeffler, Corrotect, THK, IKO, NSK and other names mentioned on this page are trademarks of their respective owners. LYDL is an independent bearing manufacturer and is not affiliated with these companies. Brand names and reference designations are used only for technical comparison and product identification.
All technical data are subject to drawing confirmation. Final bearing selection and interchangeability must be based on the approved LYDL drawing and actual operating conditions.